Color changes are a cost that finds no place in production reports. The machine does not show as "stopped", no fault record is opened — but on a line that changes color twice a shift, a significant part of the day goes on cleaning.
Added to this are the raw material spent on purge shots and the scrap among the first parts. Shortening the time often gains capacity faster than buying a new machine.
First the map: where does contamination occur?
The first thing that comes to mind at a color change is the screw and barrel. Yet colorant leaves residue at every point of the line:
| Point | Residue risk | Note |
|---|---|---|
| Conveying line (pipe, hose) | Medium | Dust and masterbatch granules remain in corners and at steps |
| Distribution table connections | Medium | The risk of a wrong connection is here too |
| Dryer hopper | High | Because material stays there for a long time, colored dust sticks to the wall |
| Dosing unit hoppers | High | Masterbatch is at its most concentrated here |
| Mixing chamber and mixer | High | Colored granulate builds up in the corners |
| Machine hopper | High | Particles catch on the conical surface |
| Screw and barrel | Highest | Dead zones and scratches hold residue |
| Hot runner | Highest | Heated material stays for a long time; if there is a dead zone, it is not cleaned out |
If any link in this chain is skipped, color contamination can come from a cleaned system even hours later — the operator blames the screw, when the source is the dryer hopper.
Order of changes: from light to dark
When production is being planned, color order is the cheapest optimization and requires no investment at all.
- When going from light to dark, cleaning is shorter; the dark color covers the remaining light residue
- Going back from dark to light is the most expensive transition — changing from black to white takes several times more purge shots
- Changing to a transparent material is the most sensitive; even the smallest residue is visible
- Staying within the same color family (light gray → dark gray) makes the transition markedly easier
Arranging the weekly production plan by color order can halve the total cleaning time for the same volume.
Hidden causes that prolong cleaning
Worn screw and barrel
Scratches on the surface and deepening clearance create places where material catches. If the same cleaning procedure takes longer than before, it is not the procedure but the surface that has changed: Screw and barrel wear
Dead zones in the hot runner
Material waits for a long time in corners where the flow stagnates. These areas cannot be swept out by purge shots; long after the color change they still send out the occasional dark streak. Setting the zone temperatures correctly and reducing dead volume in the design are essential: Hot runner control systems
Residue in the dosing unit
Masterbatch is the point in the system that carries the most concentrated color. If the dosing hopper and mixing section cannot be removed without tools, cleaning is either incomplete or takes a long time.
Wrong cleaning temperature
Raising the temperature more than necessary during purging is not always good: some materials become sticky at high temperature and cling to the surface more. It is necessary to stay within the range recommended for the purging compound being used.
More masterbatch than necessary
The safety margin left against deviation in volumetric dosing circulates more color than necessary through the system. More masterbatch means more residue: The difference between gravimetric and volumetric dosing
Equipment decisions that shorten the time
A dosing unit that can be removed without tools
Being able to remove and clean the dosing unit without tools saves time directly at a color change. A unit fixed with screws that takes a long time to dismantle is in practice never cleaned fully — the operator says "that'll do" and the residue is carried into the next color.
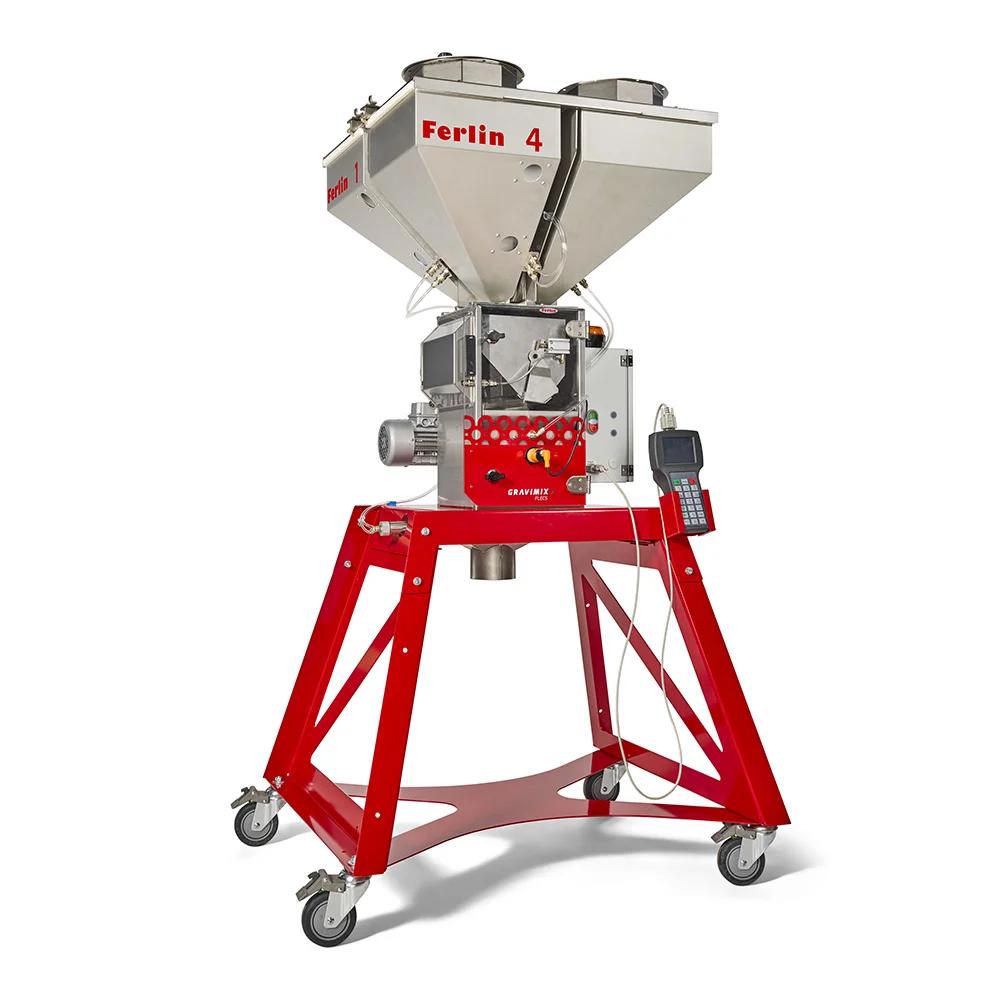
The EasyClean design on GRAVIMIX units was developed for this purpose; the unit is removed, cleaned and refitted in a short time: Gravimetric dosing systems
The right dosing ratio
Gravimetric dosing brings the masterbatch ratio down to the level actually needed. Using less color means not only raw material savings but less residue.
Line planning and coding
In central conveying it must be clear which material passes through which line. Confusion leads to a wrong material connection and to the whole batch being scrapped.
- Color coding — the lowest-cost measure
- Automatic distribution table — physically prevents a wrong connection
- Central material conveying — line cleaning is done in a planned way
A separate line or a separate unit
If there is a color produced continuously, setting aside a separate line or a separate dosing unit for it can remove the need for cleaning altogether. In plants that change color often, this is one of the fastest-returning investments.
You cannot improve what you do not measure
In most plants the color change time is known only "roughly". What needs to be measured:
1. Cleaning time — the minutes from the moment the machine stops until the first acceptable part 2. Number of purge shots and the amount of raw material spent 3. Number of scrap parts — the first parts are usually of mixed color 4. Type of transition — light to dark, or the reverse
When these four pieces of data are recorded for a few weeks, two things become clear: which transitions are really expensive, and where improvement will be most effective.
For visual defects caused by color residue: Defect troubleshooting guide
Implementation list
1. Write the cleaning procedure — which points, in what order and at what temperature are to be cleaned 2. Put the color order into the plan — the light-to-dark principle 3. Include the dryer and dosing hoppers in the procedure; these are the points skipped most often 4. Record the time and the number of shots; if there is an increase, check for equipment wear 5. Bring the masterbatch ratio down to the real need 6. Consider a separate line for frequently used colors 7. Apply coding against the risk of a wrong connection
For improvements on the dosing and conveying side, you can consult our technical support team.